Rapid Prototyping Medical | Elevate Profit Margin: 60%
Rapid prototyping medical from top prototype – factory direct sales. search top prototype, who provides innovative rapid prototyping medical. we devote to rapid prototyping medical market for several yrs.
Explore Our Top Prototype Offerings
Rapid prototyping medical from top prototype – factory direct sales. search top prototype, who provides innovative rapid prototyping medical. we devote to rapid prototyping medical market for several yrs.
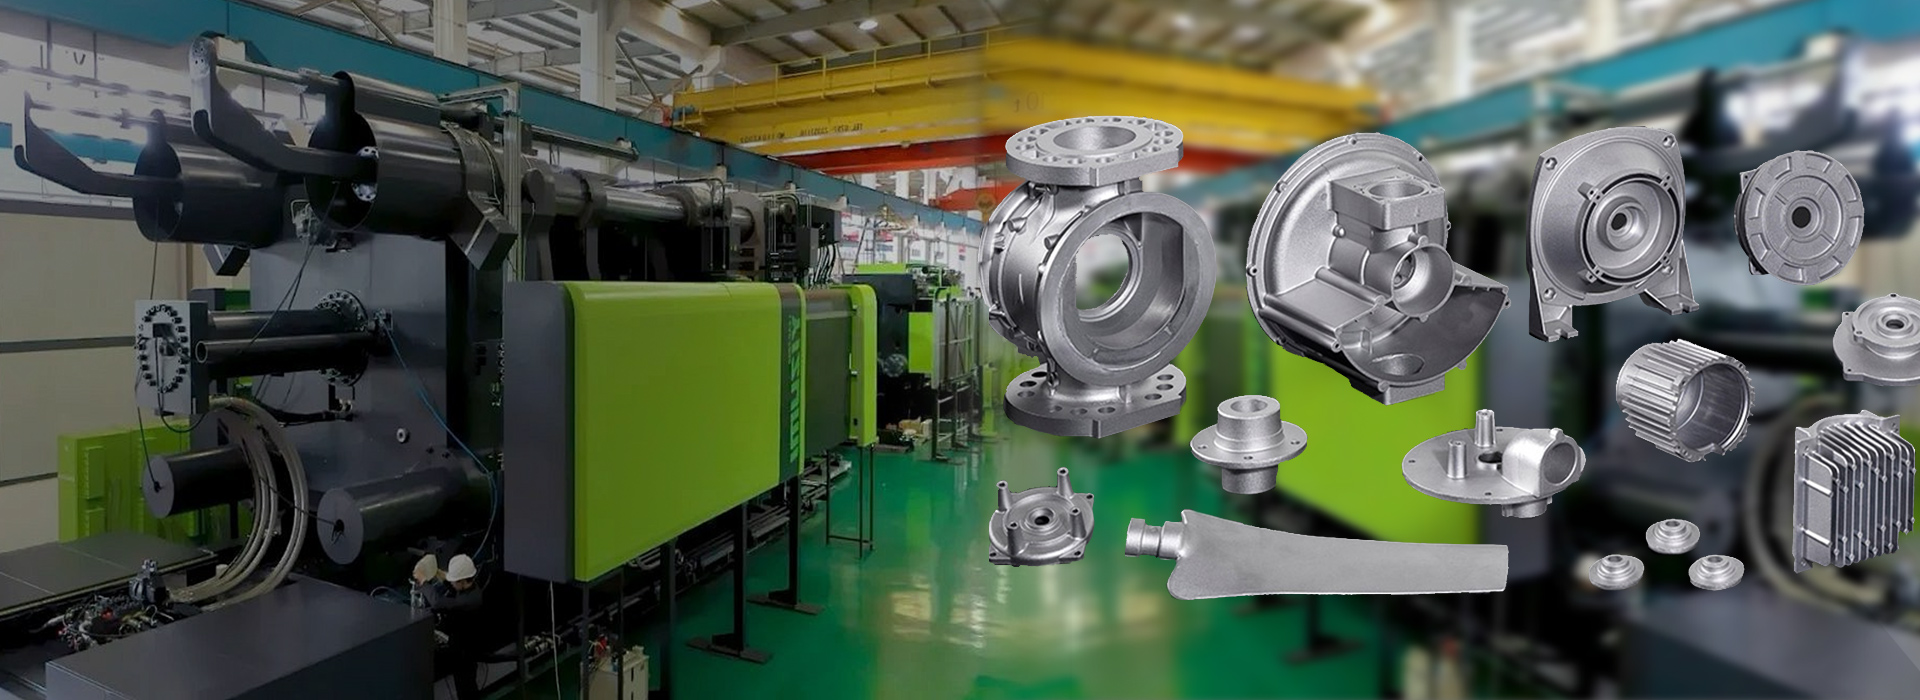
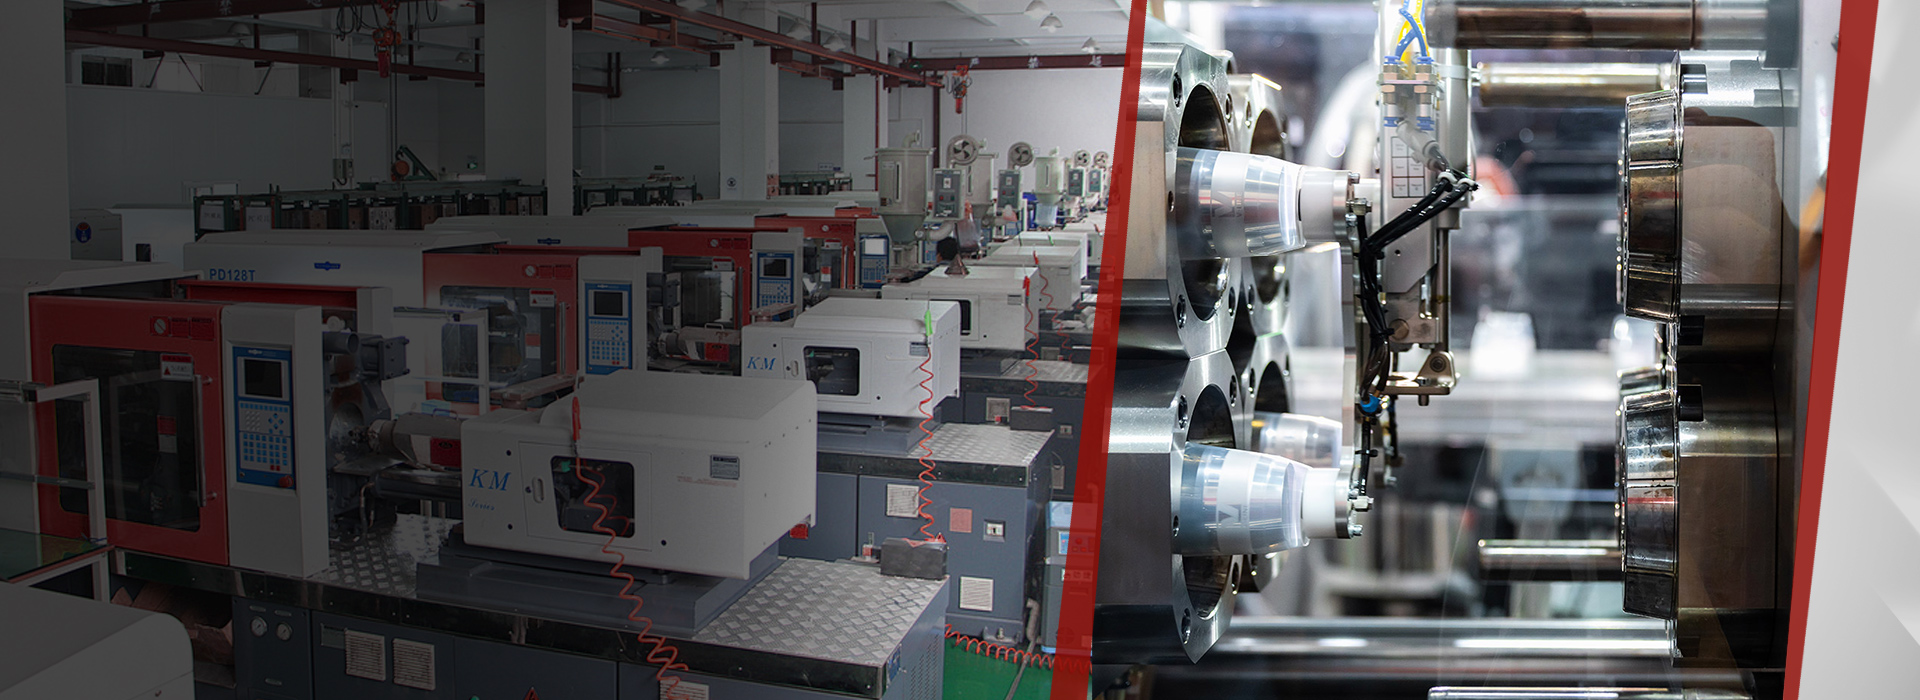

Rapid Prototyping Medical From Top Prototype: Quality You Can Trust!
Don’t miss out on TOP Prototype’s exclusive Premium rapid prototyping medical. Make TOP Prototype your trusted partner with rapid prototyping medical when searching for rapid prototyping medical.
Customer Insights On Rapid Prototyping Medical: Read Their Reviews Now!
Our commitment to quality extends to customers worldwide through our the best rapid prototyping medical.
Interested In Discovering More About Rapid Prototyping Medical?
Trust in the quality of our production not to be missed, known for their durability and ease of maintenance. Discover more on our website.
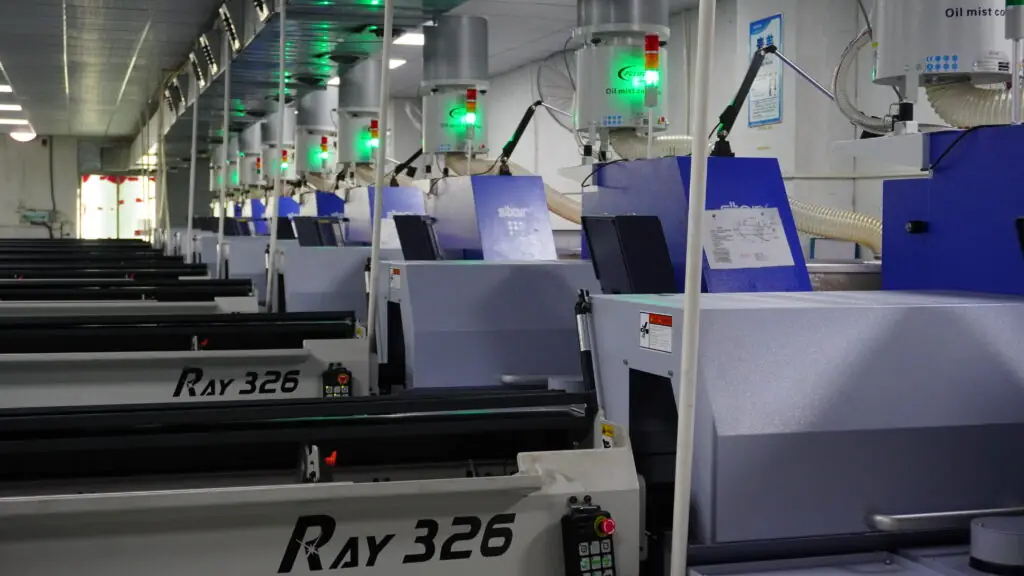
Variety
Our services range from prototype design to large-scale production, from CNC lathes to milling centers, injection molding, advanced 3D printing equipment, etc.
400,000 +
Uniquely designed parts produced 400,000 +
15 +
15 + Years in Business
What is rapid prototyping in the medical field?
Rapid prototyping in the medical field refers to the process of quickly creating physical models or prototypes of medical devices, implants, or anatomical structures using computer-aided design (CAD) and additive manufacturing technologies. This approach allows for faster iterations and improvements in design.
How does rapid prototyping benefit the development of medical devices?
Rapid prototyping benefits the development of medical devices by reducing the time and cost associated with bringing a product to market. It allows for quick testing and validation of designs, which can lead to better functionality and patient outcomes.
What technologies are commonly used in rapid prototyping for medical applications?
Common technologies used in rapid prototyping for medical applications include 3D printing (such as SLA, SLS, and FDM), CNC machining, and laser cutting. These technologies enable the creation of complex geometries and customized solutions tailored to specific medical needs.
Can rapid prototyping be used for patient-specific solutions in healthcare?
Yes, rapid prototyping can be used for patient-specific solutions in healthcare. For example, 3D printing can create customized implants, prosthetics, and surgical tools that are tailored to the unique anatomy of individual patients, improving surgical outcomes and patient satisfaction.
Learn More About Rapid Prototyping Medical With Top Prototype!
With a focus on rapid prototyping medical, TOP Prototype offers comprehensive resources to deepen your understanding and application.
TOP Prototype CNC Machining of Composite Materials
TOP Prototype CNC Machining of Composite Materials Composite materials have emerged as a crucial part of modern manufacturing due to their exceptional properties. TOP Prototype‘s expertise in CNC machining of these materials allows for the creation of precise and complex components with high performance. Let’s explore some common composite materials and their characteristics, along with
What is wire cutting? Process and application description
What is wire cutting? Process and application description Lathes and milling machines are often associated with machining, but line discharge machining (EDM) offers special advantages for certain applications. Wire-cut machining is an electrothermal process that uses electrical discharges to shape conductive materials so that complex designs can be created. The technology is widely used in
Tapped Holes vs Threaded Holes – Differences and Comparison
Tapped Holes vs Threaded Holes – Differences and Comparison In mechanical manufacturing, assembly, and precision engineering, internal threaded holes serve as the “connective tissue” of components, enabling secure fastening, precise positioning, and stable load transmission. Tapped holes and threaded holes, two widely applied types of internal threaded structures, are often conflated due to their overlapping functional goals. Yet their divergence in processing principles, structural integrity, and practical performance is substantial—differences that directly affect product reliability, production costs, and service life. This article systematically distinguishes the two, enriches the discussion with industrial practices and material science facts, simplifies complex terminology, and reconstructs the logical framework to clarify their characteristics, advantages, and application boundaries for engineering practitioners. 1. Definitions and Core Structural Traits 1.1 Tapped Holes: Direct Thread Formation in Base Material A tapped hole is an internal threaded hole formed by the tapping process, where a specialized cutting tool (tap) cuts or forms threads on the inner wall of a pre-drilled pilot hole. Unlike indirect threading methods, tapped holes integrate threads directly into the workpiece’s base material—no auxiliary inserts or reinforcements are involved. Taps operate on a subtractive principle: they remove excess material from the pilot hole’s inner surface to form standardized thread profiles, such as metric (M series), unified coarse (UNC), or unified fine (UNF) threads, with precision grades ranging from 2B (general purpose) to 3B (high precision) for imperial threads. This integration with the base material means tapped holes’ performance is inherently tied to the workpiece’s material properties. For instance, in medium-carbon steel (e.g., 45# steel) or 6061 aluminum alloy—materials with moderate ductility and strength—tapped holes deliver reliable thread retention. They are widely adopted in scenarios where the workpiece itself can bear fastening loads, avoiding the need for additional components. 1.2 Threaded Holes: A Broad Category with Indirect Threading Dominance The term “threaded hole” is a generic concept encompassing all holes with internal threads, including tapped holes. In industrial practice, however, it primarily refers to holes where threads are formed indirectly—most commonly via threaded inserts. These inserts, made of high-strength materials like 304 stainless steel or titanium alloy, are installed into pre-drilled holes to provide the internal thread interface, decoupling thread performance from the workpiece’s base material. Beyond insert-based threading, threaded holes also include structures formed by thread rolling, casting, or injection molding. Thread rolling, for example, is used for high-volume production of ductile materials like copper or low-carbon steel, forming threads through plastic deformation rather than cutting. Cast or molded threaded holes are integral to composite parts (e.g., glass-fiber reinforced plastic) or plastic components, where threads are pre-designed in the mold to eliminate post-processing. 2. Core Differences in Processing Principles and Operations The fundamental gap between tapped holes and threaded holes lies in their thread formation mechanisms—each dictating processing efficiency, precision limits, and material applicability. Simplifying these mechanisms reveals why each is preferred in specific scenarios. 2.1 Tapped Holes: Two-Step Subtractive Processing Tapping follows a rigid two-step workflow: first, drilling a pilot hole with a diameter strictly matched to the target thread (e.g., a 6.8mm pilot hole for an M8×1.25 tap); second, cutting threads using a hand tap (for small batches or manual operations) or machine tap (for automated production on CNC lathes, milling machines, or dedicated tapping centers). Critical process parameters directly impact thread quality: tap speed (typically 10-30 m/min for steel, 20-50 m/min for aluminum), feed rate (matched to thread pitch to avoid thread distortion), and lubrication (cutting oil for ferrous metals, cutting fluid for non-ferrous metals to reduce friction and prevent burring). Brittle materials like gray cast iron (HT200) or zirconia ceramic require specialized spiral-flute taps to evacuate chips and avoid cracking, while ductile materials like copper demand straight-flute taps for smooth chip removal. 2.2 Threaded Holes: Indirect Formation with Diversified Methods Insert-based threaded holes, the most common type, follow a three-step process: drilling a hole matching the insert’s outer diameter (e.g., a 10.2mm hole for an M8 helical insert), installing the insert via pressing, self-tapping, or adhesive bonding, and verifying thread accuracy. Helical wire inserts (HeliCoils), for example, are coiled stainless steel wires with a diamond cross-section—when installed, they expand to lock into the pre-drilled hole, distributing fastening loads over a larger surface area to prevent thread stripping. Other threading methods for threaded holes have clear niche applications: thread rolling achieves higher thread strength (up to 30% higher than cut threads due to work hardening) and is used for high-volume parts like automotive bolts; casting/molding eliminates post-processing but is limited to parts with simple thread geometries, as complex threads may cause mold release issues. 3. Performance Comparison and Practical Application Scenarios Evaluating strength, precision, cost, and maintainability reveals the practical trade-offs between tapped holes and threaded holes. Grounded in industrial data and real-world cases, this comparison helps engineers make evidence-based selections. 3.1 Strength and Load-Bearing Capacity Tapped holes’ load capacity is material-dependent: in high-strength alloys (e.g., 40CrNiMoA steel), a properly tapped M10 hole can withstand a tensile load of approximately 15-20 kN, meeting the needs of heavy machinery. However, in soft materials like PVC plastic or thin-walled aluminum (wall thickness < 2mm), tapped threads strip easily—even with moderate loads. Threaded holes with inserts resolve this limitation: a 304 stainless steel insert in a PVC workpiece boosts thread tensile strength by 5-8 times, enabling repeated fastening without damage. For applications requiring frequent assembly/disassembly (e.g., tooling fixtures), inserts extend service life by 3-5 times compared to tapped holes, as worn inserts can be replaced without reworking the entire part. 3.2 Precision and Dimensional Consistency Tapped holes can achieve high precision with high-quality taps and automated equipment, but tool wear introduces variability. A carbide tap for steel, for example, maintains precision for 5,000-8,000 holes before thread pitch deviation exceeds ±0.01mm. Threaded holes with inserts offer superior consistency: inserts are manufactured to ISO 898-1 standards, with thread pitch tolerance controlled within ±0.005mm. This level of precision is non-negotiable in aerospace (e.g., aircraft engine components) and medical devices (e.g., surgical instrument fasteners), where thread misalignment can lead to catastrophic failures. 3.3 Cost and Production Efficiency For low-to-medium batches (100-10,000 parts), tapped holes are 30-50% more cost-effective: the process requires only a drill press ($500-$2,000) and taps ($10-$50 each), with no additional material costs. Automated tapping centers boost high-volume efficiency, processing up to 1,000 holes per hour. Threaded holes with inserts incur higher upfront costs—inserts cost $0.5-$5 each, plus installation tools ($500-$1,500)—but reduce long-term costs for critical parts. For example, in automotive plastic bumpers, replacing a stripped tapped hole would require scrapping the bumper ($50-$100), while replacing an insert costs less than $2. 3.4 Typical Application Cases Tapped holes dominate in scenarios where base material strength suffices: automotive engine blocks (cast iron or aluminum) use tapped holes for bolt fastening, machinery frames (steel) rely on them for structural connections, and consumer electronics (aluminum housings) adopt them for component assembly. Threaded holes with inserts are preferred for soft materials (plastic enclosures, magnesium alloys), thin-walled parts (aircraft aluminum panels), critical applications (aerospace fasteners, implantable medical devices), and parts requiring maintenance (industrial tooling, marine equipment). 4. Misconception Correction and Selection Framework 4.1 Common Misconceptions Debunked Myth 1: “Tapped holes and threaded holes are identical.” Fact: Tapped holes are a subset of threaded holes, but industrial terminology reserves “threaded holes” for insert-based or non-tapped structures. Myth 2: “Tapped holes are always weaker.” Fact: In high-strength metals, tapped holes match or exceed insert-based threaded holes in load capacity—an M10 tapped hole in 40Cr steel outperforms an insert in aluminum. Myth 3: “Tapping is simpler than insert installation.” Fact: Tapping requires stricter process control (speed, feed, lubrication), while insert installation is more standardized and less prone to human error. 4.2 Practical Selection Guidelines Engineers should prioritize five core factors: 1) Material: Choose tapped holes for high-strength metals (steel, alloy aluminum); inserts for soft materials (plastic, magnesium) or thin walls. 2) Load: Tapped holes for moderate static loads; inserts for heavy loads or repeated dynamic loads. 3) Precision: Inserts for aerospace/medical high-precision needs; tapped holes for general-purpose applications. 4) Batch Size: Tapped holes for low-to-medium batches; inserts for high-volume critical parts. 5) Maintainability: Inserts for parts requiring repair; tapped holes for one-time assembly components. Tapped holes and insert-based threaded holes are not competing technologies but complementary solutions tailored to different engineering needs. Tapped holes excel in cost-effectiveness and simplicity for strong materials and moderate demands, while threaded holes with inserts deliver superior strength, precision, and maintainability for soft materials, thin walls, and critical applications. By grasping their processing differences, performance trade-offs, and application boundaries—backed by material science facts and industrial practices—engineers can optimize part design, enhance product reliability, and balance production costs. In the end, the right choice hinges on aligning the hole type with the workpiece’s material, load requirements, production scale, and service goals.
Everything You Need to Know about Multi-Axis Machining
CNC machining has come a long way over the years, from basic 2D cutting to advanced multi-axis machining that handles complex shapes with high precision and speed. As product designs get more advanced, multi-axis machining plays a key role in meeting modern manufacturing needs. That said, in this blog, we’ll explain the basics, main components,
Precision at the Core: CNC Machining for Automotive Engine Blocks by TOP Prototype
Precision at the Core: CNC Machining for Automotive Engine Blocks by TOP Prototype The engine block is the backbone of every automotive powertrain. It houses critical components, such as cylinders, crankshafts, and pistons. It bears extreme temperatures, pressure, and mechanical stress. Its precision directly determines engine efficiency, durability, and performance. Modern automotive manufacturing relies on
Bearing type: Characteristics and applications
Bearing type: Characteristics and applications If we break down rotating mechanical devices, systems or mechanisms, the different movements of their components are essential to their function. For example, blades rotate around the hub of a wind turbine to generate electricity. Do you know which devices or components control and indicate the desired movement within a
More About Rapid Prototyping Medical & Top Prototype
Our experienced R&D team is here to provide you with professional support, feel free to tell us your special requests or concerns, each product has been professionally certified to meet industry standards. We believe in: precision defines our every move, trust paves our way to success. We strongly think that we will do superior and far better. Seeing is Believing, want far more info? Give us a chance, give you a surprise. TOP Prototype collaborates with many factories and qualitified team to provide expert and affordable rapid prototyping medical to global customers. Over the past few years, our factory absorbed and digested integrated advanced technologies, exceeding the industry standard. We are looking forward to cooperating with you and providing our best services for you, as well as our rapid prototyping medical, Aerospace Manufacturing,SWISS LATHE PROCESSING. We are eager to cooperate with foreign companies which care much on the high quality, competitive prices, organizational reputation. The rapid prototyping medical will supply to all over the world, such as West Asia, South Africa, Mexico, Eastern Europe, etc.
Other Categories From Top Prototype
Why Choose Top Prototype Rapid Prototyping Medical ?
Rapid prototyping in the medical field represents a transformative approach to the development of healthcare solutions. This innovative technique allows for the swift creation of tangible models from digital designs, enabling healthcare professionals to visualize and assess medical devices, surgical instruments, and even anatomical structures with remarkable precision. By merging cutting-edge technologies such as 3D printing with a collaborative design process, rapid prototyping accelerates the journey from concept to clinical application. This not only fosters creativity and experimentation but also enhances patient outcomes by facilitating tailored solutions to complex medical challenges. Ultimately, rapid prototyping stands at the forefront of medical innovation, reshaping the landscape of healthcare delivery.
Ease Of Construction Of Rapid Prototyping Medical
Rapid prototyping in the medical field stands at the intersection of innovation and practicality, enabling swift translation of theoretical designs into tangible solutions. The ease of construction offered by advanced 3D printing and other prototyping technologies allows medical professionals to quickly create and iterate on complex models, devices, and implants. This expedites the development process, ensuring that theoretical concepts can be tested and refined within a fraction of the traditional timelines, ultimately enhancing patient care and advancing medical research.
Rapid Prototyping Medical Cost-Effectiveness
- Cost-Effectiveness: Rapid prototyping reduces costs by minimizing the need for extensive materials and labor during the initial phases of product development.
- Time Efficiency: Accelerates the design process, enabling quicker iterations and faster time-to-market for medical devices.
- Enhanced Collaboration: Facilitates communication among stakeholders, including engineers, designers, and healthcare professionals, through visual prototypes.
- Patient-Centric Design: Allows for the creation of customized solutions tailored to specific patient needs, improving the overall effectiveness of medical treatments.
- Theoretical Basis: Grounded in solid principles of design thinking and engineering, ensuring prototypes are not only practical but also innovatively aligned with medical standards.
Environmental Impact From Top Prototype
- Resource Efficiency: Rapid prototyping minimizes waste by using only the necessary materials, reducing excess production.
- Material Innovation: Encourages the development of biocompatible and sustainable materials, enhancing environmental responsibility.
- Reduced Time-to-Market: Accelerates the introduction of medical devices, allowing for quicker responses to health needs without prolonged resource use.
- Energy Consumption: Streamlined manufacturing processes generally consume less energy compared to traditional methods.
- Localized Production: Facilitates on-demand manufacturing, decreasing transportation emissions and supporting local economies.
- Lifecycle Assessment: Promotes better understanding of product lifecycle impacts, leading to more informed design decisions.
4 thoughts on “Rapid Prototyping Medical”
I got the rapid prototyping medical product today, and I must say, it totally exceeded my expectations! The quality is fantastic, the texture feels great, and it’s super practical. I definitely recommend picking one up!
We spent quite a while checking out the rapid prototyping medical products from different sellers, and it definitely paid off. Regardless of their approach or anything else, it turned out to be really awesome!
Their rapid prototyping medical products are super affordable right from the start, they’re really lightweight, and you can usually get the job done in one go!
Their rapid prototyping medical products are usually great, and they’re a breeze to manage when in use.
Comments are closed.